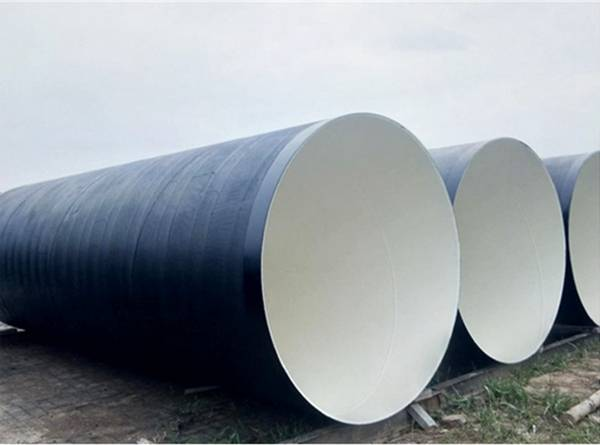
Applicable Temperature Range Of Coal-Tar Epoxy Anticorrosive Steel Pipe
In accordance with SY/T 0447‑2014 Technical Standard for Epoxy Coal‑Tar Coating of Buried Steel Pipelines, combined with coating material mechanism, on‑site engineering practice and long‑term ageing law of anti‑corrosion coating, the applicable temperature range of coal‑tar epoxy anticorrosive steel pipe is defined precisely from four dimensions: long‑term operating temperature of conveyed medium, transient peak temperature, low‑temperature resistance of ambient environment and construction ambient temperature. These four indicators shall not be confused.
First comes the long‑term operating temperature of medium conveyed inside the pipeline. The coal‑tar epoxy anti‑corrosion coating belongs to the epoxy‑modified coal‑tar pitch system. Its physical properties are significantly affected by temperature. The pitch component tends to soften and creep under high‑temperature conditions, and the adhesive force of cross‑linked resin structure decays. The standard clearly specifies that the temperature of medium conveyed for coal‑tar epoxy coating shall not exceed 80 °C. Nevertheless, this value represents the maximum limit specified in the standard, rather than the recommended temperature for long‑term operation. From the perspective of anti‑corrosion durability, the long‑term continuous conveying medium temperature of the pipeline shall be controlled within the range of ‑30 °C to 70 °C. When the medium operates persistently between 70 °C and 80 °C, the anti‑corrosion coating will age rapidly, accompanied by softening, blistering and delamination of paint film. The bonding strength between glass‑fiber cloth and coating declines, and the anti‑corrosion insulation performance degrades, raising the corrosion risk of steel pipe. Therefore, the temperature range of 70‑80 °C can only serve as an emergency working condition for an extremely short period and must not be adopted for year‑round operation.
The second parameter is transient peak temperature. Under infrequent and short‑duration working conditions, the coating can withstand a short‑term maximum temperature of 80 °C. If the medium temperature quickly falls back below 70 °C after short‑time high‑temperature exposure, no permanent damage will occur to the coating. Repeated cyclic impact of 80 °C high temperature is strictly prohibited. Alternation between hot and cold will cause repeated expansion and contraction of the anti‑corrosion coating, resulting in fatigue cracks. Corrosive media and moisture may penetrate to the steel substrate along cracks and trigger coating failure.
Thirdly, the low‑temperature resistance performance. Fully cured qualified coal‑tar epoxy anti‑corrosion coating features excellent low‑temperature toughness. When buried underground, it can endure a minimum ambient soil temperature of ‑30 °C without easy cracking or peeling under frost heave in cold regions. This low‑temperature index refers to the finished coating’s tolerance to surrounding soil temperature after burial, instead of the permissible temperature for on‑site painting construction.
Finally, the ambient temperature for anti‑corrosion coating application. Coal‑tar epoxy paint is a two‑component chemically curable coating, and ambient temperature directly determines its curing reaction rate. The optimal construction temperature ranges from 10 °C to 35 °C for sufficient curing reaction and dense film formation. The minimum allowable construction ambient temperature is 5 °C. Below 5 °C, the curing reaction speed of epoxy resin drops sharply. The paint film remains uncured for a long time and is liable to absorb dust and moisture, which will lead to permanent defects in anti‑corrosion layer. Open‑air construction at low temperature is forbidden without heating and thermal‑insulation measures.
For engineering selection, pipelines conveying hot‑water or thermal media at a persistent temperature above 70 °C shall not adopt coal‑tar epoxy external anti‑corrosion. Alternative high‑temperature‑resistant anti‑corrosion systems such as 3‑layer polyethylene (3PE) or fusion‑bonded epoxy powder shall be selected to guarantee the designed service life of pipelines.
 English
 Arabic
 Dutch
 French
 German
 Italian
 Korean
 Spanish
Leave a Reply
Want to join the discussion?Feel free to contribute!