Key Operating Points For Roll Grooving Of Plastic-Coated Steel Pipes
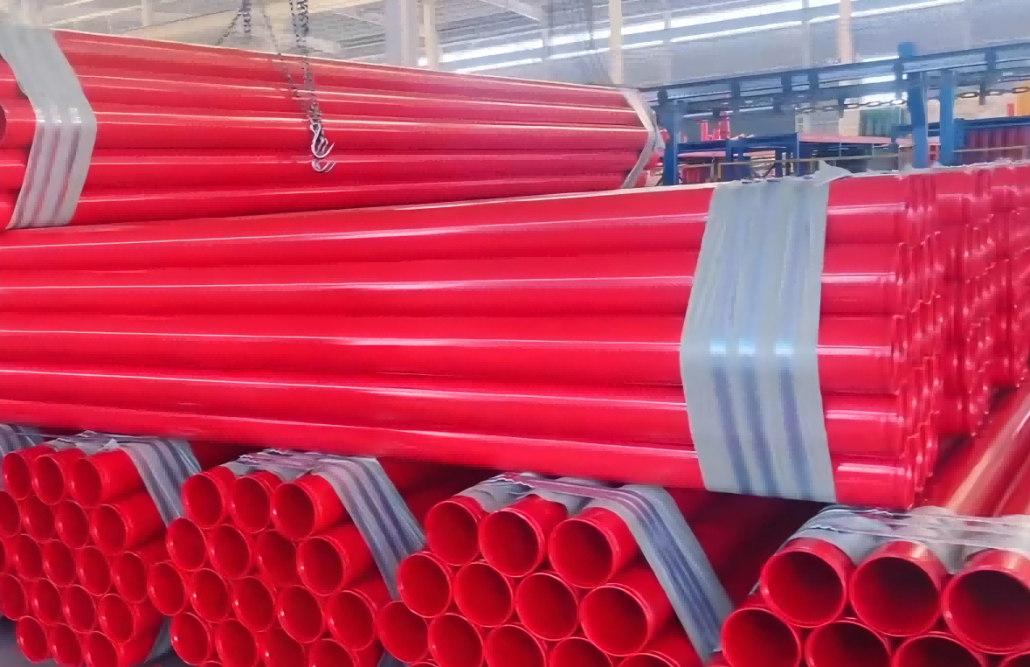
Roll grooving is a critical process for grooved connection of plastic-coated steel pipes, which directly determines the sealing performance and structural safety of piping systems. In accordance with CJ/T 156 Grooved Pipe Couplings and CJ/T 120 Water Supply Plastic-Coated Composite Steel Pipes, this article elaborates on the full-process professional operation requirements, with emphasis on coating protection and dimensional accuracy control.
Pre-operation Preparation
Equipment Selection and Inspection
Adopt dedicated roll grooving machines for plastic-coated steel pipes to avoid coating damage caused by ordinary grooving equipment. Inspect the matching degree between rolling wheels and pipe diameters, tightness of the hydraulic system and reliability of power grounding. Run the machine with no load for 30 seconds to confirm normal operation of all components and vent the oil pump to stabilize hydraulic pressure. Prepare standard groove depth gauges, vernier calipers (precision: 0.02 mm) as well as coating repair tools and materials.
Pipe Pre-treatment
Use mechanical cutting only; flame cutting is strictly prohibited. Ensure the pipe end is perpendicular to the pipe axis, with the perpendicularity deviation no more than 1 mm for DN ≤ 100 mm pipes and 1.5 mm for DN > 125 mm pipes. Remove all burrs and flashes on pipe ends, and chamfer sharp inner and outer edges to prevent scratches on rubber seals and internal/external coatings. Mark the grooving position (normally 10–15 mm away from the pipe end) as required by couplings, and keep weld seams downward and away from the grooving area. Thoroughly clean oil stains and dust on the outer pipe wall and ensure the surface is dry before grooving.
Core Grooving Operation & Parameter Control
Clamping and Positioning
Place the steel pipe horizontally on the machine support base, adjust the position to guarantee coaxial alignment between the pipe and rolling wheels, and keep the pipe perpendicular to the machine stop surface. Fasten the pipe firmly without looseness. Install an adjustable tail support to prevent bending and deformation of long pipe sections.
Progressive Roll Grooving (Key for Coating Protection)
Start the machine and press down the operating handle slowly and evenly. Control the feed rate within 0.2 mm per pipe revolution; rapid pressurization is forbidden. Continuously spray special water-based coolant during grooving to reduce friction heat and protect the plastic coating. After the limit nut is fully seated, let the pipe rotate for another 2–3 revolutions to form a uniform and smooth groove. Inspect the coating status throughout the process, and stop operation immediately once coating peeling or cracking is found.
Dimensional Tolerance Requirements
| Nominal Diameter (DN, mm) | Groove Depth (mm) | Groove Width (mm) | Allowable Deviation |
| 65 | 2.1±0.2 | 13±0.5 | ±0.2 mm |
| 100 | 2.2±0.2 | 15±0.5 | ±0.2 mm |
| 150 | 2.5±0.2 | 18±0.5 | ±0.2 mm |
| 200 | 2.8±0.2 | 20±0.5 | ±0.2 mm |
The groove depth shall never exceed 1/3 of the pipe wall thickness, so as to avoid weakening structural strength and penetrating the anti-corrosion coating.
Quality Inspection and Coating Repair
Dimensional Inspection
Measure the full-circle groove depth with a standard depth gauge to ensure uniform dimensions. Check groove width and distance from pipe end by vernier calipers, and all deviations shall comply with specifications. The groove bottom shall be flat without depressions, and groove walls shall be free of scratches and cracks.
Coating Integrity Inspection
Use high-intensity lighting to check for micro-cracks and peeling on the groove and adjacent coating areas. For damaged sections, conduct repair as follows: clean the damaged area, polish the surface with abrasive paper, apply special epoxy repair compound (coating thickness ≥ 0.5 mm), and allow natural curing for 24 hours. Coat pipe ends with sealant to prevent corrosive medium intrusion.
Visual Acceptance
No burrs or curling edges are allowed around grooves. The pipe roundness deviation shall not exceed 1% of the nominal diameter without obvious elliptical deformation. No indentations that may impair sealing performance are permitted.
Special Working Conditions and Safety Regulations
When the ambient temperature is below 5 ℃, the plastic coating becomes brittle. Reduce the grooving speed by 50%, and preheat the pipe (max. 40 ℃) to prevent coating cracking. Never pry the pipe with sharp tools; handle grooved pipes gently and avoid dropping. Keep the sealing surface free of oil to prevent accelerated aging of rubber gaskets.
Operators shall wear protective gloves and goggles. Ensure reliable grounding of the grooving machine; the hydraulic pressure shall not exceed the rated value of the equipment. Release pressure completely before dismounting pipes after shutdown.
Common Defects and Countermeasures
| Defect | Root Cause | Solutions |
| Coating peeling | Excessive pressure or fast feed rate | Reduce operating pressure and control feed rate below 0.2 mm per revolution |
| Excessive groove depth | Misadjusted limit nut | Recalibrate the limit nut and monitor depth with a gauge in real time |
| Water leakage at joint | Uneven groove depth or rough groove surface | Re-groove to ensure uniform depth and smooth surface |
| Pipe deformation | Unstable support or large pipe diameter | Add auxiliary tail supports; conduct segmented grooving for large-diameter pipes |
 Spanish
 English
 Arabic
 Dutch
 French
 German
 Italian
 Korean
Dejar un comentario
¿Quieres unirte a la conversación?Siéntete libre de contribuir!