Standards And Applications of Food-Grade FBE
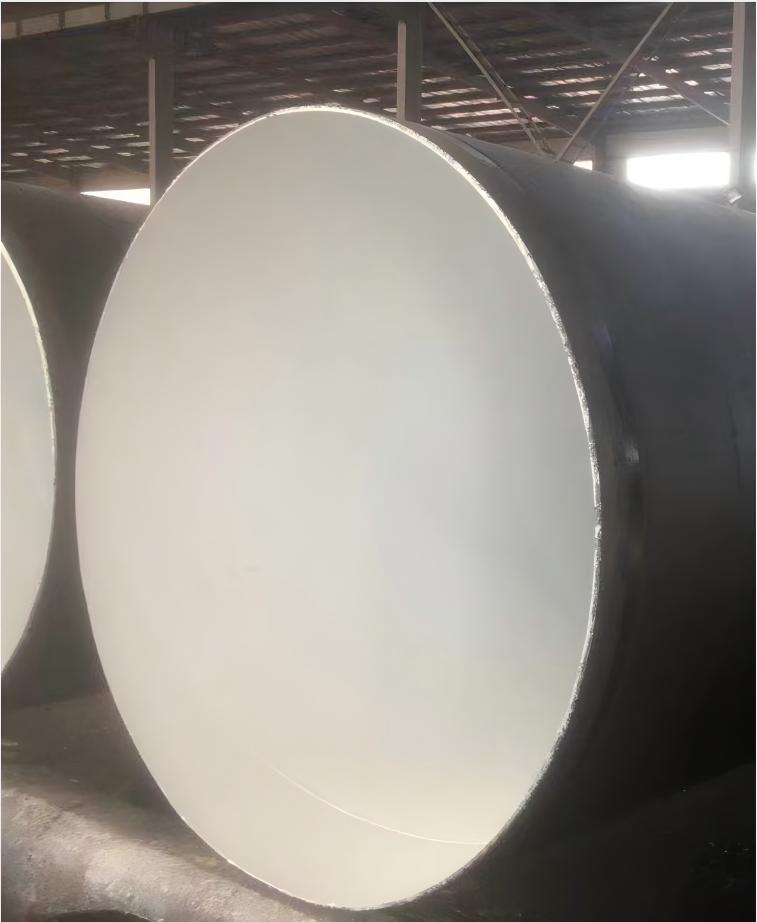
Food-grade FBE is a food-contact epoxy powder coating that is electrostatically sprayed at room temperature and fused/cured at high temperatures (above 180°C). It features non-toxicity, corrosion resistance, a smooth and easy-to-clean surface, and resistance to microbial growth. Widely used in industries with strict hygiene requirements such as food, beverage, and pharmaceutical manufacturing, it provides reliable protection for equipment and pipelines while ensuring food safety.
Core Standard Systems
Food-grade FBE must comply with both basic safety standards and coating-specific standards, and obtain authoritative certifications to be used in food-contact scenarios.
Chinese National Standards
| Standard Number | Standard Name | Core Requirements |
| GB 4806.1-2016 | National Food Safety Standard – General Safety Requirements for Food Contact Materials and Articles | Sensory requirements (no peculiar odor, no discoloration), migration limits (total migration ≤ 10mg/dm²), heavy metal limits (lead ≤ 0.01mg/kg, cadmium ≤ 0.002mg/kg) |
| GB 4806.10-2025 (Upcoming Implementation) | National Food Safety Standard – Coatings and Coatings for Food Contact Use | Replaces the current GB 4806.10-2016, implements hierarchical control based on food contact categories (Category I – direct contact with liquid food, Category II – contact with solid food), and strengthens raw material access and full-process control |
| GB/T 18593-2010 | Corrosion Protection Coating of Fusion Bonded Epoxy Powder Coatings | Specifies physical performance requirements for FBE coatings, such as thickness (generally 150-300μm), adhesion (cross-cut test ≥ Grade 1), and degree of curing (≥ 95%) |
| GB 31604.1-2021 | National Food Safety Standard – General Principles for Migration Tests of Food Contact Materials and Articles | Regulates the selection of food simulants (3% acetic acid for aqueous foods, isooctane for oily foods), temperature (≤ 120°C), and time conditions for migration tests |
International Authoritative Standards/Certifications
| Standard/Certification | Issuing Authority | Core Requirements |
| FDA 21 CFR 177.300 | U.S. Food and Drug Administration (FDA) | Specifically for polymer coatings on metal and electroplated products (including epoxy resins), requiring no release of substances hazardous to health or affecting food sensory properties. Applicable to inner walls of food processing machinery, conveyor belt coatings, etc. |
| NSF/ANSI 61 | National Sanitation Foundation (NSF) | Certification for drinking water system components, requiring no migration of harmful substances to ensure drinking water safety. Food-grade FBE must pass this certification for use in drinking water transmission pipelines. |
| NSF/ANSI 51 | National Sanitation Foundation (NSF) | Certification for food equipment materials, requiring compliance with food hygiene requirements and resistance to microbial growth. Applicable to FBE coatings for food processing equipment. |
Industry-Specific Standards
CJ/T 120-2016: Technical Specification for Fusion Bonded Epoxy Powder Coatings on Inner Walls of Steel Pipes for Urban Water Supply (applicable to drinking water distribution pipelines)
AWWA C213: American Water Works Association Standard (specifies application requirements for FBE coatings in drinking water pipelines)
CSA Z245.20: Canadian Standards Association Standard (provides detailed guidelines for FBE application and testing)
Key Technical Requirements
In addition to safety standards, food-grade FBE must meet the following technical indicators:
| Technical Indicator | Required Value | Test Method | Significance |
| Laagdikte | 150-300μm | Magnetic Thickness Gauge | Ensure sufficient corrosion resistance and mechanical strength |
| Adhesion | ≥ Grade 1 (Cross-Cut Test) | GB/T 9286 (equivalent to ISO 2409) | Prevent coating detachment and food contamination |
| Degree of Curing | ≥ 95% | Differential Scanning Calorimetry (DSC) | Ensure chemical stability of the coating and prevent migration of uncured components |
| Surface Roughness | Ra ≤ 1.6μm | Surface Roughness Tester | Smooth surface facilitates cleaning and reduces microbial growth |
| Chemical Resistance | Resistant to acids, alkalis (pH 2-12), and food processing cleaners | Immersion Test | Adapt to chemical corrosion in food processing environments |
| Hygienic Performance | Complies with GB 4789.2-2016 (no pathogenic bacteria) | Microbial Culture Test | Ensure food contact safety |
Main Application Scenarios
With its properties of non-toxicity, corrosion resistance, and easy cleaning, food-grade FBE is widely used in the food industry:
Food Processing Industry
Transmission Pipelines: Used for transporting liquid foods such as fruit juice, milk, beer, and sauces. Prevents pipeline corrosion and food contamination, while the smooth surface reduces food residue and microbial growth.
Processing Equipment: Coatings for inner walls of food processing machinery, reactors, storage tanks, and conveyor belts. Resists acid-base corrosion and high-temperature cleaning in food processing environments.
Packaging Equipment: Coatings for can and beverage can production lines, ensuring food hygiene and safety during the packaging process.
Beverage and Drinking Water Industry
Drinking Water Pipelines: Urban tap water and direct drinking water transmission pipelines. Certified by NSF/ANSI 61 to ensure safe and odor-free drinking water.
Beverage Production Lines: Coatings for pipelines and equipment in carbonated drinks, tea drinks, and bottled water production lines. Resists corrosion from carbon dioxide and acidic beverages.
Pharmaceutical and Health Product Industry
Pharmaceutical Water Systems: Purified water and water for injection transmission pipelines. Complies with GMP requirements, preventing microbial contamination and adsorption of pharmaceutical ingredients.
Health Product Production Equipment: Pipelines and reaction equipment for nutrient oral liquids and health product raw materials, ensuring product purity and hygienic safety.
Other Applications
Food-Grade Valves and Fittings: Connectors such as valves, flanges, and elbows used in food and beverage production lines. Prevents corrosion and leakage at connection points.
Food-Grade Storage Tanks: Inner wall coatings for storage tanks used to store food raw materials, semi-finished products, and finished products. Extends tank service life and ensures food quality.
Core Advantages of Food-Grade FBE
Food Safety Assurance: Certified by authoritative bodies such as FDA and NSF, with no migration of harmful substances, complying with food contact material safety requirements.
Excellent Corrosion Resistance: Resists acids, alkalis, salt spray, and corrosion from food processing chemicals, extending equipment service life.
Hygienic and Easy to Clean: The smooth surface (Ra ≤ 1.6μm) reduces food residue and microbial growth, facilitating CIP (Clean-in-Place) and SIP (Sterilize-in-Place).
High Mechanical Strength: Strong adhesion to metal substrates, impact resistance, and wear resistance, adapting to mechanical stress in food processing environments.
Environmental Sustainability: Powder coatings have no solvent emissions, complying with environmental requirements. With a long service life, they reduce waste generation.
Key Points for Compliant Use
Certification Selection: Choose appropriate certifications based on application scenarios (NSF/ANSI 51 for food equipment, NSF/ANSI 61 for drinking water systems, FDA 21 CFR 177.300 for exports to the U.S.).
Coating Thickness Control: Ensure coating thickness is within the 150-300μm range. Too thin a coating affects corrosion resistance, while too thick a coating may cause cracks.
Curing Quality Assurance: Curing temperature must reach above 180°C with a curing degree of ≥ 95% to avoid migration of uncured components into food.
Regular Inspection and Maintenance: Periodically check coating integrity and repair damages promptly to prevent exposure and corrosion of metal substrates.
Core Standard Systems
Food-grade FBE must comply with both basic safety standards and coating-specific standards, and obtain authoritative certifications to be used in food-contact scenarios.
Chinese National Standards
| Standard Number | Standard Name | Core Requirements |
| GB 4806.1-2016 | National Food Safety Standard – General Safety Requirements for Food Contact Materials and Articles | Sensory requirements (no peculiar odor, no discoloration), migration limits (total migration ≤ 10mg/dm²), heavy metal limits (lead ≤ 0.01mg/kg, cadmium ≤ 0.002mg/kg) |
| GB 4806.10-2025 (Upcoming Implementation) | National Food Safety Standard – Coatings and Coatings for Food Contact Use | Replaces the current GB 4806.10-2016, implements hierarchical control based on food contact categories (Category I – direct contact with liquid food, Category II – contact with solid food), and strengthens raw material access and full-process control |
| GB/T 18593-2010 | Corrosion Protection Coating of Fusion Bonded Epoxy Powder Coatings | Specifies physical performance requirements for FBE coatings, such as thickness (generally 150-300μm), adhesion (cross-cut test ≥ Grade 1), and degree of curing (≥ 95%) |
| GB 31604.1-2021 | National Food Safety Standard – General Principles for Migration Tests of Food Contact Materials and Articles | Regulates the selection of food simulants (3% acetic acid for aqueous foods, isooctane for oily foods), temperature (≤ 120°C), and time conditions for migration tests |
International Authoritative Standards/Certifications
| Standard/Certification | Issuing Authority | Core Requirements |
| FDA 21 CFR 177.300 | U.S. Food and Drug Administration (FDA) | Specifically for polymer coatings on metal and electroplated products (including epoxy resins), requiring no release of substances hazardous to health or affecting food sensory properties. Applicable to inner walls of food processing machinery, conveyor belt coatings, etc. |
| NSF/ANSI 61 | National Sanitation Foundation (NSF) | Certification for drinking water system components, requiring no migration of harmful substances to ensure drinking water safety. Food-grade FBE must pass this certification for use in drinking water transmission pipelines. |
| NSF/ANSI 51 | National Sanitation Foundation (NSF) | Certification for food equipment materials, requiring compliance with food hygiene requirements and resistance to microbial growth. Applicable to FBE coatings for food processing equipment. |
Industry-Specific Standards
CJ/T 120-2016: Technical Specification for Fusion Bonded Epoxy Powder Coatings on Inner Walls of Steel Pipes for Urban Water Supply (applicable to drinking water distribution pipelines)
AWWA C213: American Water Works Association Standard (specifies application requirements for FBE coatings in drinking water pipelines)
CSA Z245.20: Canadian Standards Association Standard (provides detailed guidelines for FBE application and testing)
Key Technical Requirements
In addition to safety standards, food-grade FBE must meet the following technical indicators:
| Technical Indicator | Required Value | Test Method | Significance |
| Laagdikte | 150-300μm | Magnetic Thickness Gauge | Ensure sufficient corrosion resistance and mechanical strength |
| Adhesion | ≥ Grade 1 (Cross-Cut Test) | GB/T 9286 (equivalent to ISO 2409) | Prevent coating detachment and food contamination |
| Degree of Curing | ≥ 95% | Differential Scanning Calorimetry (DSC) | Ensure chemical stability of the coating and prevent migration of uncured components |
| Surface Roughness | Ra ≤ 1.6μm | Surface Roughness Tester | Smooth surface facilitates cleaning and reduces microbial growth |
| Chemical Resistance | Resistant to acids, alkalis (pH 2-12), and food processing cleaners | Immersion Test | Adapt to chemical corrosion in food processing environments |
| Hygienic Performance | Complies with GB 4789.2-2016 (no pathogenic bacteria) | Microbial Culture Test | Ensure food contact safety |
Main Application Scenarios
With its properties of non-toxicity, corrosion resistance, and easy cleaning, food-grade FBE is widely used in the food industry:
Food Processing Industry
Transmission Pipelines: Used for transporting liquid foods such as fruit juice, milk, beer, and sauces. Prevents pipeline corrosion and food contamination, while the smooth surface reduces food residue and microbial growth.
Processing Equipment: Coatings for inner walls of food processing machinery, reactors, storage tanks, and conveyor belts. Resists acid-base corrosion and high-temperature cleaning in food processing environments.
Packaging Equipment: Coatings for can and beverage can production lines, ensuring food hygiene and safety during the packaging process.
Beverage and Drinking Water Industry
Drinking Water Pipelines: Urban tap water and direct drinking water transmission pipelines. Certified by NSF/ANSI 61 to ensure safe and odor-free drinking water.
Beverage Production Lines: Coatings for pipelines and equipment in carbonated drinks, tea drinks, and bottled water production lines. Resists corrosion from carbon dioxide and acidic beverages.
Pharmaceutical and Health Product Industry
Pharmaceutical Water Systems: Purified water and water for injection transmission pipelines. Complies with GMP requirements, preventing microbial contamination and adsorption of pharmaceutical ingredients.
Health Product Production Equipment: Pipelines and reaction equipment for nutrient oral liquids and health product raw materials, ensuring product purity and hygienic safety.
Other Applications
Food-Grade Valves and Fittings: Connectors such as valves, flanges, and elbows used in food and beverage production lines. Prevents corrosion and leakage at connection points.
Food-Grade Storage Tanks: Inner wall coatings for storage tanks used to store food raw materials, semi-finished products, and finished products. Extends tank service life and ensures food quality.
Core Advantages of Food-Grade FBE
Food Safety Assurance: Certified by authoritative bodies such as FDA and NSF, with no migration of harmful substances, complying with food contact material safety requirements.
Excellent Corrosion Resistance: Resists acids, alkalis, salt spray, and corrosion from food processing chemicals, extending equipment service life.
Hygienic and Easy to Clean: The smooth surface (Ra ≤ 1.6μm) reduces food residue and microbial growth, facilitating CIP (Clean-in-Place) and SIP (Sterilize-in-Place).
High Mechanical Strength: Strong adhesion to metal substrates, impact resistance, and wear resistance, adapting to mechanical stress in food processing environments.
Environmental Sustainability: Powder coatings have no solvent emissions, complying with environmental requirements. With a long service life, they reduce waste generation.
Key Points for Compliant Use
Certification Selection: Choose appropriate certifications based on application scenarios (NSF/ANSI 51 for food equipment, NSF/ANSI 61 for drinking water systems, FDA 21 CFR 177.300 for exports to the U.S.).
Coating Thickness Control: Ensure coating thickness is within the 150-300μm range. Too thin a coating affects corrosion resistance, while too thick a coating may cause cracks.
Curing Quality Assurance: Curing temperature must reach above 180°C with a curing degree of ≥ 95% to avoid migration of uncured components into food.
Regular Inspection and Maintenance: Periodically check coating integrity and repair damages promptly to prevent exposure and corrosion of metal substrates.
 Dutch
 English
 Arabic
 French
 German
 Italian
 Korean
 Spanish
Plaats een Reactie
Meepraten?Draag gerust bij!