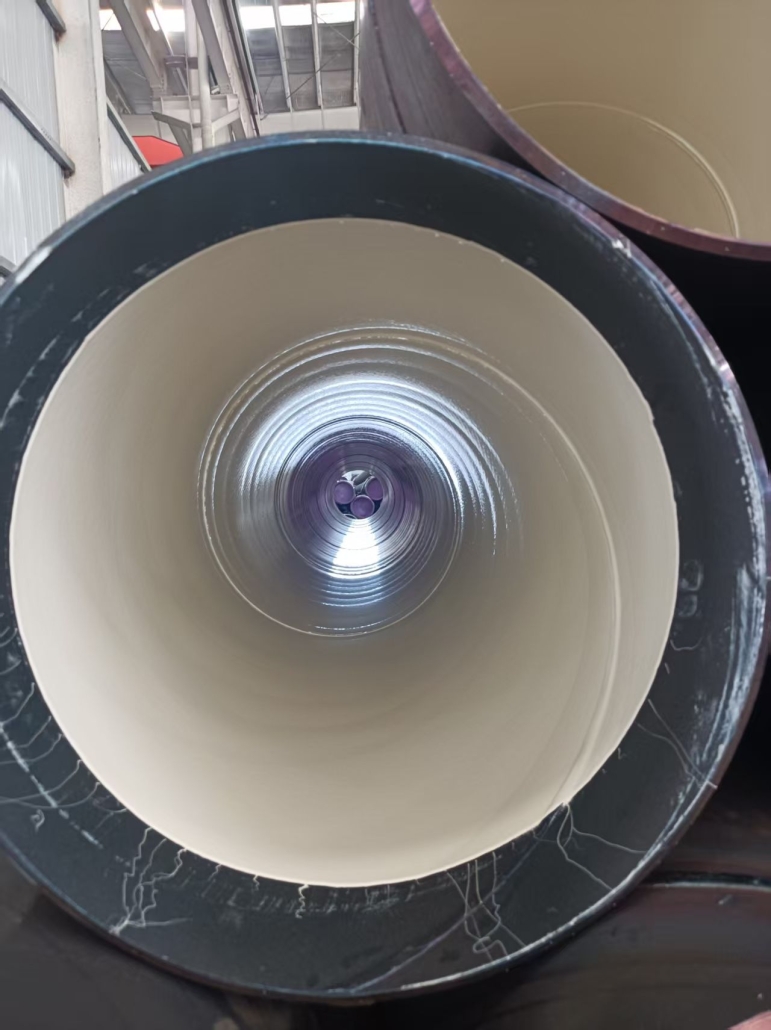
DIN 30670은 독일에서 가스 및 수도 공급을 위한 매립된 철도 파이프라인에 적용되는 폴리에틸렌 부식 방지 코팅에 관한 핵심 기술 표준입니다. 이 표준에 따른 3PE 코팅의 벗겨짐 강도 시험은 코팅과 기재물 사이의 접착성뿐만 아니라 이중층 접착성도 검증하는 데 중점을 두고 있습니다. 모든 시험 작업은 체계적인 오류 및 인적 오차를 제거하기 위해 표준 규정을 엄격히 준수해야 합니다.
표본 준비 및 조건화(준수 기준)
샘플링 및 절단 요건: 표본은 완제품의 부식 방지 파이프의 평평한 직선 부분에서 채취하여야 하며, 파이프 끝, 둘레 용접 및 결함 부위로부터 최소 50 mm 떨어져야 합니다. 코팅 띠, 구멍 또는 기계적 손상이 있는 표본은 엄격히 금지됩니다. 표본은 정밀 기계 절단으로 20mm ± 0.5mm의 표준 폭으로 준비해야 합니다. 절단 스트레스로 인해 레이어 간에 사전 탈기(pre-delamination)가 발생하지 않도록 부스러기 없는 열처리된 절단이 이루어져야 합니다. 25 ± 5 mm 크기의 미리 벗겨진 막대가 준비되어야 합니다. 이 때 표적 시험 인터페이스(FBE/강철 기판, 접착제/FBE, PE/접착제)를 손상시키지 않고 코팅 본체 또는 강철 파이프 기본 재료를 분리해야 합니다.
표본 조절 사양: 주변 온도 시험을 위해 표본은 최소 16시간 동안 23 °C ± 2 °C 및 50% ± 5% 상대 습도인 표준 환경에서 조절되어야 합니다. 상승된 온도 껍질 시험을 위해 코팅이 완전한 열 균형 상태에 도달하도록 보장하기 위해 표준 지정된 온도(예: 50 °C, 80 °C)에서 최소 45분 동안 일정한 온도 절연이 수행되어야 합니다. 테스트는 대상 온도에 도달할 때까지 시작하지 마십시오.
표본 보관 제한 사항: 준비된 표본은 빛이 들어오지 않는 안정적인 온도 환경에서 보관해야 합니다. 코팅 접착 특성의 돌연변이를 방지하기 위해 기름이나 용제에 접촉하거나 직접 고온에 노출하는 것은 엄격히 금지됩니다.
시험 장비 및 파라미터 제어(정확도 핵심 요소)
장비 교정 및 정밀도: 인장 시험기는 ISO 7500-1의 Class 1 정확도 요건을 충족해야 하며, 법적으로 교정된 힘 측정 시스템을 갖추어야 합니다. 유효 기간 내에. 폴리에틸렌 표면 코팅이 부서지지 않도록 되도록 중등도의 클램핑 힘으로 특수 비금속 슬립 방지 클램프를 사용해야 합니다.
일정한 파라미터 요구 사항: DIN 30670은 90° 껍질 벗기기 모드를 규정하며, 껍질 벗기기 각도 편차는 ≤ ±2°여야 합니다. 각도 편차는 데이터 변형을 초래하기 때문입니다. 껍질 제거 속도는 ±5 mm/min의 정확도로 100 mm/min으로 엄격하게 제어되어야 하며, 시험 중에는 시동이나 속도 변화 없이 일정한 속도로 유지되어야 합니다. 데이터 수집 주파수는 부하 변위 곡선을 완벽하게 기록하기 위해 10 Hz 이상이어야 합니다.
온도 제어 장비 요구 사항: 고온 시험용 온도 조절기는 온도 제어 정확도가 ±1 °C 이하이고, 지역적 과열이 발생하지 않아야 합니다. 또는 온도 변동. 시험 중 시료 조정을 위해 온도 조절기를 열어 사용하는 것은 시험 결과에 영향을 미치는 갑작스러운 온도 변화를 방지하기 위해 금지됩니다.
시험 운영 및 실패 결정(유효성 확인 키)
표준 클램핑 작동: 표본은 껍질 벗기기 힘의 동축적 정렬을 보장하고, 휨이나 변형이 없도록 클램핑하여 직선적인 껍질 벗기기 경로를 확보해야 합니다. 껍질 길이의 처음 50mm와 마지막 20mm는 불안정한 응력 구간으로 간주되며, 이 구간의 데이터는 버려야 합니다. 연속적이고 안정적인 중간 껍질 벗기기 구간의 데이터만 수집해야 합니다.
결함 모드 결정: DIN 30670에서는 접합부 결함이 유효한 결함 모드라고 정의합니다. 시험 결과는 무효화되며, 코팅의 조립 결함, 시편 절단 손상으로 인한 조기 벗겨짐, 클램프 미끄러짐 또는 기판 변형이 시험 중 발생하면 재시험이 필요합니다. 고장 인터페이스의 종류는 정확히 기록되어야 하며, 서로 다른 인터페이스의 껍질 벗김 성능은 별도의 그룹에서 시험 및 문서화되어야 합니다.
비동시적 시료 관리: 각 시험 그룹에는 최소 5개의 비동시적 시료가 포함되어야 합니다. 분산 계수가 > 15%인 이상한 데이터는 제외되며, 남은 유효 시료의 평균값을 최종 결과로 삼습니다.
데이터 계산 및 기록 추적성(규정 준수 보장)
데이터 계산 기준: 페일 강도는 실제 시편 폭을 기준으로 한 단위 폭당 하중으로 계산된 N/mm로 보고됩니다. 규정 준수는 DIN 30670의 온도 규정 제한치에 따라 결정됩니다. 단일 시편의 측정값은 표준 하한치의 80%보다 낮아서는 안 되며, 그룹 평균은 표준 인덱스 요건을 충족해야 합니다.
추적 가능 기록 요건: 시험 보고서는 DIN 30670 표준 개정판, 시편 번호, 장비 교정 번호, 주변 온도 및 기타 사항을 완전히 명시해야 합니다. 습도, 절연 시간, 벗겨짐 각도/속도, 고장 모드, 원시 부하 데이터 및 곡선. 시험 시료는 재검사 및 추적성을 위해 보고서 발간까지 보관해야 합니다.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2026-02-05 06:55:392026-02-05 07:04:413PE 부식 방지 코팅의 벗겨짐 강도 시험에 대한 주의사항 (DIN 30670)
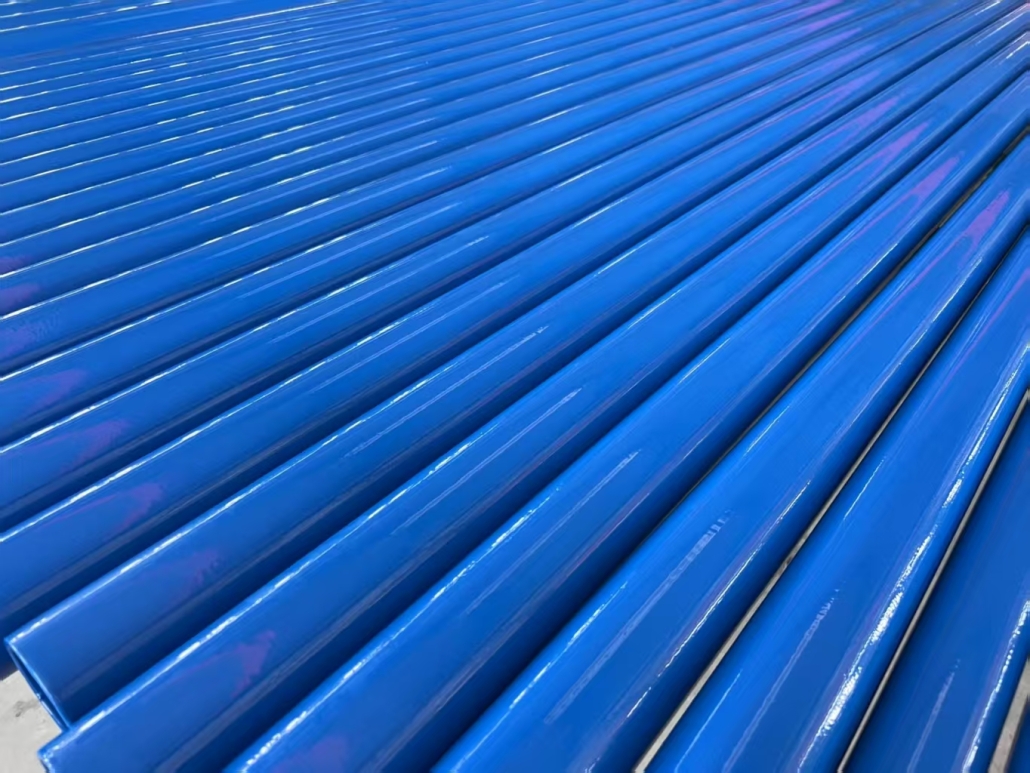
Food-grade FBE is a food-contact epoxy powder coating that is electrostatically sprayed at room temperature and fused/cured at high temperatures (above 180°C). It features non-toxicity, corrosion resistance, a smooth and easy-to-clean surface, and resistance to microbial growth. Widely used in industries with strict hygiene requirements such as food, beverage, and pharmaceutical manufacturing, it provides reliable protection for equipment and pipelines while ensuring food safety.
Core Standard Systems
Food-grade FBE must comply with both basic safety standards and coating-specific standards, and obtain authoritative certifications to be used in food-contact scenarios.
Chinese National Standards
Standard Number
Standard Name
Core Requirements
GB 4806.1-2016
National Food Safety Standard – General Safety Requirements for Food Contact Materials and Articles
Sensory requirements (no peculiar odor, no discoloration), migration limits (total migration ≤ 10mg/dm²), heavy metal limits (lead ≤ 0.01mg/kg, cadmium ≤ 0.002mg/kg)
GB 4806.10-2025 (Upcoming Implementation)
National Food Safety Standard – Coatings and Coatings for Food Contact Use
Replaces the current GB 4806.10-2016, implements hierarchical control based on food contact categories (Category I – direct contact with liquid food, Category II – contact with solid food), and strengthens raw material access and full-process control
GB/T 18593-2010
Corrosion Protection Coating of Fusion Bonded Epoxy Powder Coatings
Specifies physical performance requirements for FBE coatings, such as thickness (generally 150-300μm), adhesion (cross-cut test ≥ Grade 1), and degree of curing (≥ 95%)
GB 31604.1-2021
National Food Safety Standard – General Principles for Migration Tests of Food Contact Materials and Articles
Regulates the selection of food simulants (3% acetic acid for aqueous foods, isooctane for oily foods), temperature (≤ 120°C), and time conditions for migration tests
International Authoritative Standards/Certifications
Standard/Certification
Issuing Authority
Core Requirements
FDA 21 CFR 177.300
U.S. Food and Drug Administration (FDA)
Specifically for polymer coatings on metal and electroplated products (including epoxy resins), requiring no release of substances hazardous to health or affecting food sensory properties. Applicable to inner walls of food processing machinery, conveyor belt coatings, etc.
NSF/ANSI 61
National Sanitation Foundation (NSF)
Certification for drinking water system components, requiring no migration of harmful substances to ensure drinking water safety. Food-grade FBE must pass this certification for use in drinking water transmission pipelines.
NSF/ANSI 51
National Sanitation Foundation (NSF)
Certification for food equipment materials, requiring compliance with food hygiene requirements and resistance to microbial growth. Applicable to FBE coatings for food processing equipment.
Industry-Specific Standards
CJ/T 120-2016: Technical Specification for Fusion Bonded Epoxy Powder Coatings on Inner Walls of Steel Pipes for Urban Water Supply (applicable to drinking water distribution pipelines)
AWWA C213: American Water Works Association Standard (specifies application requirements for FBE coatings in drinking water pipelines)
CSA Z245.20: Canadian Standards Association Standard (provides detailed guidelines for FBE application and testing)
Key Technical Requirements
In addition to safety standards, food-grade FBE must meet the following technical indicators:
Technical Indicator
Required Value
Test Method
Significance
코팅 두께
150-300μm
Magnetic Thickness Gauge
Ensure sufficient corrosion resistance and mechanical strength
Adhesion
≥ Grade 1 (Cross-Cut Test)
GB/T 9286 (equivalent to ISO 2409)
Prevent coating detachment and food contamination
Degree of Curing
≥ 95%
Differential Scanning Calorimetry (DSC)
Ensure chemical stability of the coating and prevent migration of uncured components
Surface Roughness
Ra ≤ 1.6μm
Surface Roughness Tester
Smooth surface facilitates cleaning and reduces microbial growth
Chemical Resistance
Resistant to acids, alkalis (pH 2-12), and food processing cleaners
Immersion Test
Adapt to chemical corrosion in food processing environments
Hygienic Performance
Complies with GB 4789.2-2016 (no pathogenic bacteria)
Microbial Culture Test
Ensure food contact safety
Main Application Scenarios
With its properties of non-toxicity, corrosion resistance, and easy cleaning, food-grade FBE is widely used in the food industry:
Food Processing Industry
Transmission Pipelines: Used for transporting liquid foods such as fruit juice, milk, beer, and sauces. Prevents pipeline corrosion and food contamination, while the smooth surface reduces food residue and microbial growth.
Processing Equipment: Coatings for inner walls of food processing machinery, reactors, storage tanks, and conveyor belts. Resists acid-base corrosion and high-temperature cleaning in food processing environments.
Packaging Equipment: Coatings for can and beverage can production lines, ensuring food hygiene and safety during the packaging process.
Beverage and Drinking Water Industry
Drinking Water Pipelines: Urban tap water and direct drinking water transmission pipelines. Certified by NSF/ANSI 61 to ensure safe and odor-free drinking water.
Beverage Production Lines: Coatings for pipelines and equipment in carbonated drinks, tea drinks, and bottled water production lines. Resists corrosion from carbon dioxide and acidic beverages.
Pharmaceutical and Health Product Industry
Pharmaceutical Water Systems: Purified water and water for injection transmission pipelines. Complies with GMP requirements, preventing microbial contamination and adsorption of pharmaceutical ingredients.
Health Product Production Equipment: Pipelines and reaction equipment for nutrient oral liquids and health product raw materials, ensuring product purity and hygienic safety.
Other Applications
Food-Grade Valves and Fittings: Connectors such as valves, flanges, and elbows used in food and beverage production lines. Prevents corrosion and leakage at connection points.
Food-Grade Storage Tanks: Inner wall coatings for storage tanks used to store food raw materials, semi-finished products, and finished products. Extends tank service life and ensures food quality.
Core Advantages of Food-Grade FBE
Food Safety Assurance: Certified by authoritative bodies such as FDA and NSF, with no migration of harmful substances, complying with food contact material safety requirements.
Excellent Corrosion Resistance: Resists acids, alkalis, salt spray, and corrosion from food processing chemicals, extending equipment service life.
Hygienic and Easy to Clean: The smooth surface (Ra ≤ 1.6μm) reduces food residue and microbial growth, facilitating CIP (Clean-in-Place) and SIP (Sterilize-in-Place).
High Mechanical Strength: Strong adhesion to metal substrates, impact resistance, and wear resistance, adapting to mechanical stress in food processing environments.
Environmental Sustainability: Powder coatings have no solvent emissions, complying with environmental requirements. With a long service life, they reduce waste generation.
Key Points for Compliant Use
Certification Selection: Choose appropriate certifications based on application scenarios (NSF/ANSI 51 for food equipment, NSF/ANSI 61 for drinking water systems, FDA 21 CFR 177.300 for exports to the U.S.).
Coating Thickness Control: Ensure coating thickness is within the 150-300μm range. Too thin a coating affects corrosion resistance, while too thick a coating may cause cracks.
Curing Quality Assurance: Curing temperature must reach above 180°C with a curing degree of ≥ 95% to avoid migration of uncured components into food.
Regular Inspection and Maintenance: Periodically check coating integrity and repair damages promptly to prevent exposure and corrosion of metal substrates.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-12-09 08:59:032025-12-09 08:59:05식품용 FBE의 표준 및 적용
1. Core Classification and Technical Characteristics of FBE Coating Thickness
FBE coatings are categorized into three types based on thickness: Single-Layer Basic Type, Single-Layer Reinforced Type, and Dual-Layer Composite Type, with their performance increasing in a stepped manner as thickness increases:
Strong adhesion of base layer, wear/chemical corrosion resistance of top layer
Double spraying, layered functional design
2. Precise Matching of Application Scenarios by Thickness
1. Single-Layer Basic Type (300-400 μm): Conventional Corrosion Environments
Typical Scenarios:
Municipal water transmission pipelines (DN ≤ 250 mm, soil resistivity ≥ 100 Ω·m)
Underground coal mine gas extraction pipes (pressure ≤ 1.6 MPa)
Thermal power plant circulating water pipelines (water temperature ≤ 60℃)
Case Reference: The gathering and transportation pipeline network of Tarim Oilfield adopts ASTM A53 Gr.B steel pipes with 350 μm FBE coating, achieving a 98.7% coating integrity rate after 5 years.
2. Single-Layer Reinforced Type (400-500 μm): Moderately Severe Environments
Typical Scenarios:
Acid-alkali waste liquid transmission in chemical industrial parks (pH 3-11)
Buried gas pipelines in coastal areas (soil salt content ≤ 3%)
Trenchless crossing pipelines under highways (anti-rolling requirements)
Suitable Pipe Diameters: DN 250-DN 800. According to SY/T 0315, coating thickness increases with pipe diameter (e.g., ≥ 450 μm for DN 800).
3. Dual-Layer Composite Type (≥ 620 μm): Extreme Service Environments
Thickness Uniformity: Deviation ≤ ±50 μm for the same pipe section (per SY/T 0315)
Cathodic Disbondment: Immersion at 70℃ for 30 days, disbondment width ≤ 10 mm
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-10-23 03:46:572025-10-23 03:46:59다른 두께의 FBE 강관에 대한 적용 및 표준의 종합 분석
FBE steel pipes refer to Fusion Bonded Epoxy Coated Steel Pipes. Their operating temperature mainly depends on the heat resistance of the FBE coating, with the core applicable temperature range and influencing factors as follows:
I. Core Operating Temperature Range
According to industry standards for FBE coatings (e.g., GB/T 23257-2017 Polyethylene Anticorrosive Coatings for Buried Steel Pipes, and anticorrosion requirements supporting API 5L Specification for Line Pipe), the operating temperature is divided into long-term use 그리고 short-term use:
Long-term operating temperature: Generally -30℃ ~ 80℃
Within this temperature range, the FBE coating can maintain stable adhesion, impact resistance, and corrosion resistance, without cracking, peeling, or accelerated aging due to temperature changes (suitable for long-term stable working conditions such as buried water transportation, gas transmission, and ordinary chemical fluid transportation).
Short-term operating temperature: Maximum tolerance up to 120℃ (duration ≤ 1 hour)
This is only applicable to temporary working conditions (e.g., pipeline hydrostatic testing, short-term transportation of slightly high-temperature media). Exceeding 120℃ or long-term exposure to environments above 80℃ will cause the coating to soften, decrease in strength, and even lead to thermal aging failure.
II. Key Factors Affecting Operating Temperature
FBE Coating Formulation
General-purpose FBE: The upper heat resistance limit is 80℃, suitable for normal-temperature media;
High-temperature resistant FBE (modified grade): By adding heat-resistant resins (e.g., phenol-modified epoxy), the long-term operating temperature can be increased to 100℃ ~ 120℃ (suitable for working conditions such as hot oil and high-temperature sewage, requiring customized production separately).
Coating Curing Quality
Insufficient curing of the FBE coating (e.g., insufficient curing temperature or too short curing time) will result in low coating crosslinking density, significantly reduced heat resistance, and potential blistering or peeling even at 60℃ ~ 70℃.
Medium Environment
If the transported medium contains strongly corrosive substances (e.g., strong acids, strong alkalis, organic solvents), high temperatures will accelerate the chemical reaction between the medium and the coating. In such cases, the actual operating temperature should be reduced (e.g., using at normal temperature) to avoid premature coating failure.
III. Temperature Requirements for Typical Application Scenarios
Avoid local overheating of the pipe body caused by direct sunlight exposure
Municipal tap water/sewage pipelines
0℃ ~ 60℃
Prevent frost heaving at low temperatures and avoid microbial growth at high temperatures
Ordinary chemical fluid pipelines
-10℃ ~ 80℃
Adjust according to the corrosiveness of the medium; reduce to normal temperature for strongly corrosive media
Temporary pressure testing/maintenance conditions
≤120℃ (short-term)
Single duration should not exceed 1 hour; avoid frequent over-temperature
IV. Precautions
Prohibition of over-temperature use: Long-term exposure above 80℃ (for general-purpose FBE) or 120℃ (for high-temperature resistant FBE) will cause thermal aging of the coating and loss of adhesion, eventually leading to pipe rust;
Low-temperature limitation: Below -30℃, the FBE coating will become brittle and its impact resistance will decrease. Avoid external impact on the pipeline (e.g., provide cushioning protection during burial);
Selection matching: If the operating temperature exceeds 80℃, clearly require suppliers to provide “high-temperature resistant FBE coatings” and submit coating heat resistance test reports (e.g., high-temperature adhesion test, thermal aging test data).
In summary, the conventional operating temperature of FBE steel pipes is mainly -30℃ ~ 80℃. For special working conditions, adaptation can be achieved by customizing high-temperature resistant coatings or adjusting the operating temperature. The core principle is to ensure the coating maintains structural and performance stability throughout its service life.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-09-25 10:21:142025-09-25 10:21:17FBE 강관의 작동 온도
The transportation and storage of Fusion-Bonded Epoxy (FBE)-coated steel pipes are critical links in ensuring their corrosion protection performance. Although FBE coatings exhibit excellent corrosion resistance, they are relatively brittle with poor impact and scratch resistance, and are sensitive to ambient temperature, humidity, and mechanical forces. Therefore, standardized transportation and storage management is essential to prevent coating damage, aging, or structural damage to the pipes, thereby ensuring the effectiveness of subsequent construction and long-term operation. Below are the specific operational specifications:
1. Preparation Before Transportation
Before transportation, coating quality verification 그리고 protective pre-treatment must be completed to minimize the risk of damage during transportation:
1.1 Coating Quality Re-inspection
In accordance with GB/T 39636-2020 Technical Specification for Fusion-Bonded Epoxy Powder External Coatings on Steel Pipes, re-inspect the coating’s appearance (no pinholes, bubbles, or peeling), thickness (single layer ≥ 300μm, double layer ≥ 600μm), and adhesion strength (≥ 10MPa). Non-conforming products must be repaired before transportation.
Conduct a comprehensive inspection of coating integrity using a spark tester (15kV voltage) to ensure no leakage points (inspection speed ≤ 0.3m/s).
1.2 Protection of Pipe Ends
Fit plastic protective caps (HDPE material, thickness ≥ 3mm) on both ends of the pipes (beveled or flat ends) to prevent foreign objects from entering the pipe interior and avoid collision damage to the coatings at the ends.
For flanged pipes, cover the flange sealing surfaces with anti-rust film + rigid protective covers to prevent scratches or rust on the sealing surfaces.
1.3 Selection of Packaging Methods
Choose appropriate packaging based on the pipe specifications (length, diameter), with the core goal of preventing friction and collision between pipes:
Steel Pipe Type
Packaging Method
Short pipes (≤ 6m)
Bundled with steel strips (strip width ≥ 30mm, ≥ 3 bundling points). Place rubber pads or non-woven fabrics (thickness ≥ 5mm) between each bundle of pipes.
Long pipes (> 6m)
Fixed with dedicated frames (steel or wood, with soft liners attached to the inner sides of the frames). The load capacity of a single frame must not exceed the design limit.
Small-diameter pipes (≤ 200mm)
Insert into dedicated plastic pipe sleeves (length ≥ 100mm) to avoid direct contact between pipe orifices.
2. Transportation Process Control
During transportation, focus on preventing mechanical impact, friction scratches, and environmental erosion. The specific requirements are as follows:
2.1 Loading and Unloading Specifications
사용 specialized lifting equipment exclusively: Prioritize hooks and slings (width ≥ 100mm) with soft liners (rubber or nylon). Direct bundling of pipes with steel wire ropes is prohibited (to avoid indentation damage to the coating).
Control the loading/unloading speed at ≤ 0.5m/s. Throwing or impacting is prohibited. Pipes must be kept horizontal when lifted to prevent coating scratches caused by tilting.
2.2 Transportation Vehicles and Fixation
사용 flatbed trucks or dedicated tank trucks. The truck bed must be paved with non-slip rubber sheets or wooden pads (thickness ≥ 10mm) to prevent pipe sliding during transportation.
Pipe fixation methods:
For bundled short pipes: Secure them with steel strips + soft pads (a second round of fixation). Place non-woven fabrics between the steel strips and the coating to avoid direct metal contact.
For long pipes in frames: Fix the frames to the truck bed with bolts, and secure the pipes inside the frames with wedges (wooden, with soft liners attached) to prevent displacement due to jolting.
2.3 Environmental Protection Measures
Transportation in rainy weather: Pipes must be covered with rainproof tarpaulins (PVC material, thickness ≥ 0.3mm). Ventilation holes (1 hole every 5m, diameter ≥ 50mm) must be reserved on the tarpaulins to prevent condensation accumulation in the truck bed, which could dampen the coating.
Transportation in high temperatures (ambient temperature > 35℃): Cover the top of the truck bed with sunshade nets to avoid prolonged exposure of the FBE coating to sunlight (which accelerates coating aging).
Transportation in low temperatures (ambient temperature < 0℃): For long-distance transportation (> 24h), provide preheating protection for the coating surface (cover with thermal insulation cotton to prevent coating embrittlement due to low temperatures).
2.4 Transportation Routes and Speed
Prioritize smooth highways and avoid bumpy roads (e.g., unpaved roads, potholed sections). Maintain a driving speed ≤ 60km/h (≤ 80km/h on highways). Decelerate gently when turning or braking to prevent pipe impact caused by sudden stops.
3. Storage Management Specifications
The storage of FBE-coated steel pipes must meet the requirements of moisture prevention, pressure prevention, and corrosion prevention. Strictly follow the following standards for storage sites and stacking methods:
3.1 Requirements for Storage Sites
The site must have hardened ground (concrete or asphalt, flatness tolerance ≤ 5mm) with a drainage slope ≥ 3‰ to prevent water accumulation from soaking the pipes.
Keep away from corrosive environments: Prohibit placement near chemical industrial zones, salt spray areas, or sewage ditches. Set up guardrails around the site to prevent unauthorized mechanical access.
Environmental control for the site: The storage temperature should be -5℃ ~ 35℃, with relative humidity ≤ 85%. For long-term storage (> 3 months), build sunshade sheds (top height ≥ 4m) to avoid direct sunlight and rain erosion.
3.2 Stacking Methods and Load Control
Bottom support: Use wooden or concrete support blocks (height ≥ 200mm, spacing between supports ≤ 3m). Attach soft liners (rubber, thickness ≥ 10mm) to the top of the support blocks. Direct placement of pipes on the ground is prohibited.
Stacking height:
For pipes with diameter ≤ 500mm: Maximum stacking height ≤ 5 layers, with rubber pads (thickness ≥ 5mm) placed between each layer.
For pipes with diameter > 500mm: Maximum stacking height ≤ 3 layers. Mark the bottom-layer pipes separately to prevent long-term compression deformation.
Stacking spacing: Pipes of different specifications and batches must be stored in separate zones with a spacing ≥ 1m between zones. Install identification signs (indicating specifications, production date, and coating type) for easy management.
3.3 Maintenance for Long-Term Storage
Regular inspections: Daily check the coating appearance (for scratches or bubbles); weekly inspect whether the support blocks are deformed or the ground is waterlogged; monthly conduct random inspections of coating integrity using a spark tester (sampling ratio ≥ 5%).
Environmental regulation: Strengthen ventilation during the rainy season (open the side curtains of the sunshade shed). In winter, if the site temperature < -10℃, provide intermittent preheating for the pipes (use a hot air blower to blow the coating surface, controlling the temperature at 10℃ ~ 15℃ to prevent coating embrittlement).
End protection: If the plastic protective caps fall off, replace them immediately to prevent dust and moisture from entering the pipe interior and causing internal rust.
4. Common Issues and Emergency Handling
4.1 Coating Scratches During Transportation
For minor scratches (scratch area ≤ 30mm²): Upon arrival at the destination, immediately repair using a special FBE repair agent (two-component liquid epoxy). Follow the process: grinding → cleaning → application → curing. Conduct a spark test after repair.
For moderate scratches (scratch area > 30mm²): Mark the location, prohibit use, and contact the manufacturer to send professionals for on-site repair or return the pipes to the factory for handling.
4.2 Coating Blistering During Storage
Cause: Mostly due to site humidity and water ingress between the coating and the substrate.
Handling: Cut open the blistered area, remove moisture and rust, re-blast the surface (to Sa2.5 standard), apply FBE powder, and test the adhesion strength (≥ 10MPa) after curing.
4.3 Pipe Deformation
For slight bending deformation (deformation ≤ L/1000, where L is the pipe length): Straighten slowly using a dedicated straightening machine, and re-inspect the coating integrity after straightening.
For severe deformation (deformation > L/1000): Classify as scrapped and prohibit use.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-09-01 05:50:382025-09-01 05:50:40FBE 코팅 강관의 운송 및 보관
Repair of FBE anti-corrosion steel pipes (Fusion Bonded Epoxy anti-corrosion steel pipes) must comply with strict standards and specifications to ensure that the anti-corrosion performance of the repaired coating matches the original coating and guarantee the long-term operational safety of the pipeline. The following details the repair standards, repair methods, and quality inspection from three aspects:
I. Core Standards for Repair
The repair of FBE anti-corrosion coatings must refer to authoritative domestic and international standards, mainly including:
Domestic Standards
Technical Specification for Fusion Bonded Epoxy Powder External Coating of Steel Pipes (SY/T 0315-2013): Clearly specifies the repair requirements for FBE coating damage, including repair materials, surface treatment, construction processes, and inspection methods.
Technical Specification for Repair of Anti-corrosion Coatings on Buried Steel Pipes (GB/T 5135.22-2019): Provides general regulations on the repair process and quality control of anti-corrosion coatings (including FBE) for buried pipelines.
Code for Construction of Oil and Gas Pipeline Crossing Engineering (GB 50424-2015): Involves special requirements for damage repair of FBE pipelines in crossing sections.
International Standards
ISO 21809-3 Petroleum and Natural Gas Industries – Pipeline Transportation Systems – Part 3: Steel Pipe Coatings: Puts forward internationally accepted requirements for the compatibility of FBE coating repair materials and construction processes.
AWWA C213 Standard for Fusion-Bonded Epoxy Coatings for Steel Water Pipelines: Emphasizes the hygienic safety of materials for the repair of FBE coatings in drinking water pipelines.
II. Premises for Repair and Classification of Damage
Before repair, it is necessary to evaluate the type and extent of damage to determine whether repair is required:
Minor damage: Local scratches on the coating (depth ≤ 50% of coating thickness), pinholes (diameter ≤ 1mm).
Moderate damage: Local peeling of the coating (area ≤ 100cm²), scratches with depth > 50% of coating thickness but without exposing the substrate (steel pipe not exposed).
Severe damage: Large-area peeling of the coating (area > 100cm²), exposure of the substrate (direct exposure of the steel pipe), and steel pipe deformation caused by mechanical damage.
III. Specific Repair Methods
Repair must follow the process of “surface treatment → material selection → coating application”. The repair methods vary slightly according to the degree of damage:
1. Surface Treatment (Core Step)
Regardless of the type of damage, the damaged area and the surrounding 50-100mm range must be surface-treated to ensure the substrate is clean and rough, thereby enhancing the adhesion of repair materials:
Rust removal grade: For areas with exposed substrate (steel pipe exposed), the rust removal grade must reach Sa2.5 (near-white rust removal), which can be achieved by sandblasting; for non-substrate-exposed areas (only coating damage), it must reach St3 (thorough manual rust removal), which can be done using wire brushes, sandpaper, or power tools for grinding.
Cleanliness requirements: Remove rust, oil, dust, and old coating debris from the surface, clean it with dry compressed air or a lint-free cloth, and ensure the surface moisture content is ≤ 4%.
2. Selection of Repair Materials
Repair materials must be compatible with the original FBE coating (chemical stability and adhesion matching) and meet anti-corrosion performance requirements:
Minor damage (pinholes, shallow scratches): Two-component epoxy repair paint (such as solvent-free epoxy coating) is used, with a dry film thickness ≥ 150μm (equivalent to the thickness of the original FBE coating).
Moderate damage (local peeling, deep scratches): Modified epoxy repair paste (paste-like, can be thickly applied) or FBE repair powder (requires heat curing, suitable for high-demand scenarios) is used, with a dry film thickness ≥ 200μm.
Severe damage (substrate exposure, large-area peeling): First apply an epoxy primer (dry film thickness ≥ 80μm), then apply a repair coating of the same type as the original FBE (such as high-build epoxy coating), with a total dry film thickness ≥ 300μm (not less than the thickness of the original coating).
3. Coating Application
Manual application: Suitable for small-area damage (< 100cm²). Use a scraper or brush to evenly apply the repair material to the treated surface, ensuring no bubbles or sagging, and the edges transition smoothly with the original coating (avoiding steps).
Heat curing: If FBE repair powder is used, the repair area must be preheated to 180-220℃ (consistent with the curing temperature of the original FBE) using a heat gun or medium-frequency heating equipment, then the powder is sprayed and allowed to cool and cure naturally.
Multi-layer application: For areas requiring higher thickness (such as severe damage), 2-3 layers of coating must be applied, with an interval of ≥ 4 hours between each layer (after thorough drying) to avoid cracking caused by excessive thickness of a single layer.
IV. Quality Inspection Standards
After repair, the following inspections must be conducted to ensure qualification:
Appearance: The coating surface is flat, without bubbles, pinholes, or sagging, and connects smoothly with the original coating, with no obvious color difference.
두께: Detected with a coating thickness gauge, the dry film thickness is not less than that of the original FBE coating (usually ≥ 300μm), and the local minimum thickness is not less than 80% of the design value.
Adhesion: Using the cross-cut test (grid spacing 1mm, coating peeling ≤ 5% after tape peeling) or the pull-off test (adhesion ≥ 5MPa, consistent with the original coating).
Pinhole detection: Detected with a spark tester (voltage set according to thickness: 15-30kV for 100-300μm), with no breakdown (no sparks).
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-08-05 08:34:322025-09-01 03:35:44FBE 부식 방지 강관에 대한 수리 표준 및 방법
FBE (Fusion Bonded Epoxy) anti-corrosion steel pipes use steel pipes as the matrix, and the epoxy powder is melted and cured on the surface of the steel pipes through high-temperature spraying to form an anti-corrosion layer. To improve the service life of FBE anti-corrosion steel pipes, efforts can be made in multiple links such as production and manufacturing, transportation and storage, installation and use, and later maintenance:
Production and Manufacturing Link
Optimize Steel Pipe Pretreatment: The cleanliness and roughness of the steel pipe surface directly affect the adhesion of the FBE coating. Before coating, shot blasting or sandblasting is used to thoroughly remove impurities such as rust, oil stains, and oxide scales on the steel pipe surface, so that the steel pipe surface reaches Sa2.5 level (near-white level), and the roughness is controlled at 40 – 100μm. Appropriate roughness can increase the contact area between the coating and the steel pipe, enhance adhesion, reduce the risk of coating peeling, and prolong the service life.
Strictly Control the Coating Process: Precisely control the spraying temperature, thickness, and curing time of the epoxy powder. Generally, the spraying temperature is 230 – 250℃, the coating thickness is controlled at 300 – 500μm according to the requirements of the use environment, and the curing time needs to ensure that the powder is completely melted and cross-linked and cured. A stable coating process can ensure that the coating is uniform, dense, and free of defects such as pinholes and bubbles, effectively blocking the intrusion of corrosive media.
Select High-Quality Raw Materials: Select reliable-quality epoxy powder to ensure that it has good chemical corrosion resistance, water resistance, weather resistance, and mechanical properties. High-quality epoxy powder can maintain stable anti-corrosion performance for a long time in different environments. At the same time, the quality of the steel pipe itself is also crucial. Select steel pipes that meet relevant standards, have uniform wall thickness, and excellent material quality to reduce corrosion problems caused by defects of the steel pipes themselves.
Transportation and Storage Link
Strengthen Protective Packaging: During transportation, use appropriate packaging materials for FBE anti-corrosion steel pipes, such as wrapping with plastic film or protective sleeves specially for anti-corrosion pipes, to prevent damage to the coating due to collision and friction between steel pipes. For long-distance transportation, soft pads should be laid at the bottom of the carriage, and the steel pipes should be fixed to avoid coating damage caused by transportation bumps.
Reasonably Plan Storage: The storage site should be a dry and well-ventilated place to avoid the steel pipes being in a humid environment for a long time. The steel pipes should be stored elevated, keeping a certain distance from the ground to prevent the coating from being eroded by ground moisture. At the same time, direct sunlight should be avoided to prevent the coating from aging due to ultraviolet radiation and shortening the service life.
Installation and Use Link
Standardize Installation Operations: During the installation process, strictly follow the operating procedures, avoid pulling and bending the steel pipes with force, and prevent the coating from cracking or peeling due to excessive force. Use appropriate connection methods. For example, when welding, protective measures should be taken to prevent welding spatter from damaging the coating. For coating damage caused during the installation process, it should be repaired in a timely manner to ensure the integrity of the anti-corrosion layer.
Control the Use Environment: Try to avoid using FBE anti-corrosion steel pipes in harsh environments such as extreme temperatures, high humidity, and strong acids and alkalis. If unavoidable, additional protective measures can be taken, such as adding an insulating layer and a protective sleeve outside the pipeline, to reduce the erosion of the environment on the coating. At the same time, parameters such as the temperature, 酸碱度 (acidity and alkalinity), and flow rate of the conveying medium should be controlled to reduce the corrosion effect of the medium on the steel pipes and the coating.
Later Maintenance Link
Regular Detection and Evaluation: Establish a regular detection system, and use technical means such as ultrasonic detection and leak point detection to check the integrity, adhesion of the FBE coating, and the corrosion of the steel pipes. Through regular detection, potential problems can be found in a timely manner, and corresponding repair measures can be taken to prevent the problems from expanding.
Timely Repair the Coating: Once problems such as coating damage and aging are found, the coating should be repaired in a timely manner. According to the degree of coating damage, select an appropriate repair method. For example, for small-area damage, manual brushing or spraying of epoxy repair paint can be used; for large-area damage, re-FBE coating treatment is required.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-07-16 10:28:072025-07-16 10:28:09FBE 부식 방지 강관의 수명을 향상시키는 방법은 무엇입니까?
FBE (Fusion-Bonded Epoxy) anticorrosive coating inspection standards encompass international, national, and industry specifications, focusing primarily on coating performance parameters and acceptance requirements. Below is a detailed overview of the core standard systems and key technical indicators:
I. International Standard System
ISO 21809 Series
ISO 21809-1:2018: Specifies that the FBE primer layer thickness in 3-layer polyethylene (3LPE)/polypropylene (3LPP) coatings shall be ≥300μm, with adhesion ≥5MPa.
ISO 21809-11:2019: Requires field joint and repair coatings to match the original coating thickness and pass the cathodic disbondment test (65°C, 28 days) with a disbondment distance ≤10mm .
ISO 12944-6: Salt spray testing (ISO 9227) mandates that FBE coatings withstand 1,000 hours of testing without blistering or rusting .
ASTM Standards
ASTM D4541-22: Adhesion testing requires a pull-off strength ≥5MPa and a loading rate of 0.8MPa/s ±10% .
ASTM G42-11: High-temperature cathodic disbondment testing (80°C, 0.5MPa) allows a maximum disbondment distance of ≤15mm .
ASTM A 775/A 775M: General standard for epoxy coatings, specifying requirements for coating thickness, adhesion, and continuity.
NACE SP0169-2024
Coating insulation resistance ≥10,000Ω·m², with a cathodic protection potential ≤-0.85V (vs CSE) .
II. Chinese National Standards
GB/T 39636-2020 (Core Standard)
두께: Single-layer FBE: 350μm ±50μm; double-layer FBE: total thickness ≥600μm, with local minimum thickness ≥80% of the design value.
Cathodic Disbondment: Disbondment distance ≤15mm after testing at 65°C for 28 days .
GB/T 4956-2003
Thickness measurement accuracy for magnetic substrates: ±10μm, with at least 3 measurements per square meter .
GB/T 5210-2006
Pull-off test requires a specimen diameter of 20mm ±0.5mm and surface preparation to Sa2.5 grade.
III. Industry Standards
SY/T 4113.11-2023 (Replacing SY/T 0063-1999)
Holiday Detection: High-voltage spark testing voltage calculated as V = 7900\sqrt{T} (T = thickness in mm), with a typical value of 2.1kV (0.4mm thickness) and a holiday density ≤2 defects/m² .
Low-Voltage Detection: DC voltage ≤100V, used to detect thickness deficiencies .
SY/T 0315-97
Double-layer FBE total thickness ≥600μm, requiring passage of a 1.5J impact test and 3° bend test without disbondment .
SY/T 7036-2016
Compatibility requirements for coatings and cathodic protection in oil and gas station pipelines: current density ≤10μA/cm² .
IV. Special Scenario Standard Requirements
High-Temperature Environments
Hot oil pipelines must pass the ASTM G42 test (80°C, 0.5MPa) with a disbondment distance ≤15mm .
Glass transition temperature (Tg) must exceed 80°C, verified via DSC testing.
Buried Pipelines
Coating insulation resistance ≥10,000Ω·m², with a cathodic protection potential ≤-0.85V (vs CSE).
Combined with Close Interval Potential Survey (CIPS) to assess defect distribution.
Repair Projects
Repaired areas must meet thickness, adhesion, and holiday detection requirements, with interface bond strength ≥4MPa.
V. Surface Preparation and Calibration Specifications
Surface Preparation Standards
Sandblasting cleanliness grade must reach Sa2.5 (GB/T 8923.1) or SSPC-SP 10 (near-white grade).
Equipment Calibration
Thickness Gauges: Calibrated using standard test blocks (e.g., 350μm ±5μm), with an error ≤±5%.
Spark Testers: Verified daily using calibration plates with artificial defects, ensuring voltage error ≤±2%.
Reporting Requirements
Test data must include location, equipment model, calibration records, and bear CMA/CNAS accreditation stamps.
Through this standard system, the thickness, adhesion, corrosion resistance, and compatibility with cathodic protection of FBE anticorrosive coatings can be comprehensively evaluated, ensuring long-term reliability in oil & gas, chemical, and other industrial applications.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-06-04 07:39:202025-06-04 07:39:21FBE 부식 방지 코팅에 대한 검사 기준
During the heat treatment process of steel pipes, various defects may occur due to improper process parameters, equipment failures, or operational errors. The following is a detailed analysis of common defects and their preventive measures:
I. Defects in the Heating Stage
Oxidation and Decarburization Defect manifestation: An oxide scale (Fe₃O₄, Fe₂O₃) forms on the surface of the steel pipe, and the loss of carbon elements leads to a decrease in surface hardness. Cause: Excessive air (oxidizing atmospheres such as O₂, H₂O, etc.) in the heating furnace, too high a heating temperature, or too long a holding time. Preventive measures: Use a controlled atmosphere furnace (such as N₂, Ar protective gas, or drip methanol and acetone to generate a protective atmosphere). Coat the surface of the workpiece with an anti-oxidation coating (such as a borax coating). Strictly control the heating temperature and time to avoid overheating.
Coarse Grain (Overheating) Defect manifestation: The austenite grains grow excessively, resulting in a decrease in mechanical properties (reduction in toughness and plasticity). Cause: The heating temperature exceeds the critical temperature by a large margin (for example, overheating occurs when the quenching heating temperature is 50~80℃ higher than the Ac3 line), or the holding time is too long. Preventive measures: Accurately set the heating temperature (according to the process specifications of the steel grade, for example, the quenching temperature of 45 steel is 840±10℃). Adopt stepwise heating or rapid heating technology to reduce the residence time at high temperatures. For overheated workpieces, they can be reprocessed through normalizing (to refine the grains).
II. Defects in the Cooling Stage
Quenching Cracks Defect manifestation: Transgranular cracks appear on the surface or inside of the workpiece, mostly occurring at the sudden change of the cross-section, sharp corners, or holes. Cause: The cooling rate is too fast (for example, when carbon steel is cooled below the Ms point, the martensitic transformation generates huge internal stress). The workpiece design is unreasonable (in stress concentration areas), it is not preheated, or there is machining stress before quenching. The cooling medium is not properly selected (for example, alloy steel is prone to cracking when quenched in brine). Preventive measures: Improve the structure of the workpiece (round off sharp corners, avoid large differences in thickness), and carry out stress-relieving annealing before quenching. Adopt isothermal quenching (bainitic transformation) or step quenching (first quench into a medium above the Ms point and hold it, then cool it slowly). Select an appropriate cooling medium (for example, 40Cr steel should be cooled in oil instead of water), and control the temperature of the quenching medium (for example, the oil temperature should not be lower than 40℃).
Insufficient or Uneven Hardness Defect manifestation: The surface or core hardness does not reach the standard, or the hardness difference in the same cross-section is >5HRC. Cause: Insufficient heating temperature (incomplete austenitization), insufficient holding time. Insufficient cooling rate (for example, the aging of the quenching medium and a large amount of impurities lead to a decrease in the cooling capacity). Surface decarburization (resulting in a lower hardness after quenching). Preventive measures: Strictly calibrate the temperature control instrument to ensure uniform heating temperature (the furnace temperature uniformity is ≤±5℃). Regularly replace or filter the quenching medium (for example, when the water content in the oil is >5%, the water needs to be removed). Control decarburization (the same as the oxidation prevention measures), and perform surface carburizing compensation if necessary.
III. Defects in the Tempering Stage
Tempering Brittleness Defect manifestation: The toughness decreases after low-temperature tempering (200~300℃) (the first type of tempering brittleness), or brittleness occurs during slow cooling after high-temperature tempering (450~650℃) (the second type of tempering brittleness). Cause: The first type: Carbides precipitate along the grain boundaries during the decomposition of martensite, which is irreversible. The second type: Impurity elements such as P and Sn segregate at the grain boundaries, which is reversible (reheating and rapid cooling can eliminate it). Preventive measures: Avoid tempering in the brittle temperature range, or use rapid tempering cooling (for the second type of brittleness). Select steel grades with low impurities, or add alloying elements such as Mo and W to inhibit grain boundary segregation.
Abnormal Hardness after Tempering Defect manifestation: The hardness after tempering is higher or lower than expected (for example, insufficient hardness after high-temperature tempering after quenching, or higher hardness after low-temperature tempering). Cause: Incorrect setting of the tempering temperature (for example, mistakenly setting 500℃ as 400℃), failure of the temperature control system, or insufficient holding time. Preventive measures: Calibrate the thermocouple and temperature control instrument before tempering (with an accuracy of ±1% FS), and use a dual-sensor monitoring system. Hold according to the process requirements (generally 1~2 hours, adjusted according to the cross-sectional thickness).
IV. Overall Defects: Deformation and Dimension Out-of-Tolerance Defect manifestation: The steel pipe is bent, the ovality exceeds the standard (for example, the diameter tolerance is >±0.5%), and the straightness is >1mm/m. Cause: The self-weight of the workpiece or improper support during the heat treatment process (for example, a long steel pipe sags when heated while hanging). There is a large temperature difference in the cross-section during cooling (for example, the cooling rates of the upper and lower surfaces are uneven during horizontal quenching). Residual stress is not eliminated (for example, direct quenching of a cold-rolled pipe without annealing leads to stress superposition). Preventive measures: Use a vertical furnace to heat long steel pipes, or use supporting fixtures to keep them horizontal. During quenching, rotate or swing the workpiece to ensure uniform cooling (for example, arrange annular nozzles during spray quenching). Carry out annealing or normalizing before heat treatment to eliminate machining stress, and straighten the finished product (such as pressure straightening or tension straightening).
V. Preventive Management System
Process Standardization: Develop a “Steel Pipe Heat Treatment Process Card”, clearly defining parameters such as temperature, time, and medium (for example, the normalizing temperature of Q345B steel pipe is 880~920℃, and the holding time is 1min/mm).
Equipment Maintenance: Regularly calibrate the temperature control system (check once a week), clean the carbon deposits in the furnace (once a month), and check the stirring device of the quenching tank (ensure the flow rate ≥0.5m/s).
Process Monitoring: Use an infrared thermometer to monitor the surface temperature of the workpiece in real time, and randomly inspect the hardness (at least 3 points per pipe) and metallographic structure (for example, the martensite grade ≤3) for each batch.
Personnel Training: Operators must work with a certificate and master the heat treatment characteristics of different steel grades (for example, stainless steel solution treatment requires rapid water cooling to avoid the precipitation of the σ phase).
The core preventive idea for heat treatment defects of steel pipes is to precisely control the parameters of the three stages of heating, cooling, and tempering, and reduce stress concentration and organizational inhomogeneity. Through process optimization, equipment maintenance, and process monitoring, the defect rate can be effectively reduced, and the stability of the mechanical properties of steel pipes can be improved.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-04-18 08:11:152025-04-18 08:11:37Heat Treatment Defects Of Steel Pipes And Their Prevention
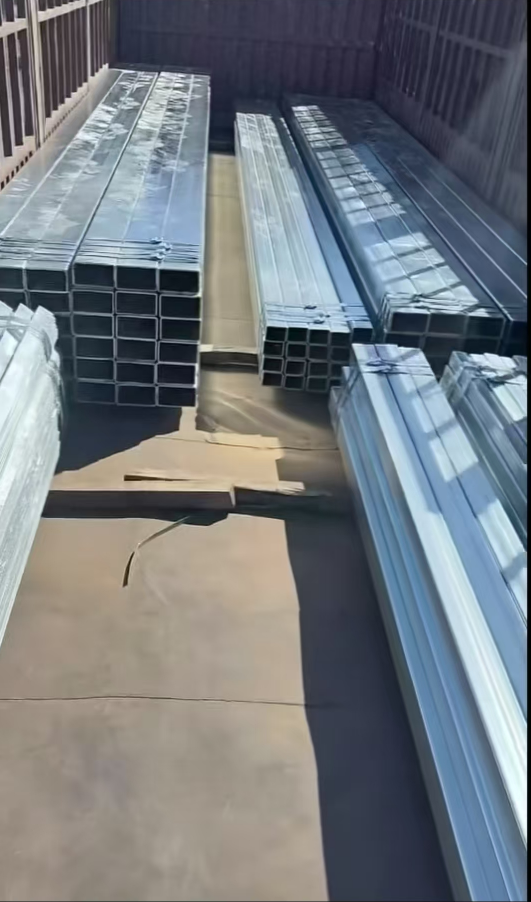
The mechanical properties analysis of galvanized pipes requires a comprehensive evaluation based on material properties, galvanizing process and application scenarios. The following is a detailed analysis based on the latest industry standards and research data:
I. Basic materials of galvanized pipes
1. Substrate type
1. Carbon steel: commonly used Q195, Q215, Q235 (corresponding to American standard ASTM A53 Grade B), yield strength 195-235MPa, tensile strength 315-430MPa.
2. Low alloy steel: such as Q345 (corresponding to ASTM A106 Grade B), yield strength ≥345MPa, tensile strength 470-630MPa.
Surface hardness: zinc coating HV (Vickers hardness) is about 50-70, significantly lower than the steel itself (Q235 HBW≈120).
Impact toughness: -20℃ Charpy V-notch impact energy ≥27J (GB/T 18984-2016), low-temperature toughness may decrease by 10-15% after galvanizing.
3. Fatigue performance
Fatigue limit: The fatigue limit of smooth specimens is about 35-45% of the tensile strength. Defects in the galvanized layer (such as microcracks) may reduce the fatigue life by 15-20%.
III. Effect of process on performance
1. Hot-dip galvanizing
Advantages: The zinc layer and the substrate form a Fe-Zn alloy layer (thickness 5-15μm), and the bonding force is ≥35N/cm (GB/T 2694-2018).
Disadvantages: High temperature (450℃) treatment may cause grain coarsening and a decrease in elongation of 5-8%.
2. Electrogalvanizing
Advantages: No high temperature effect, maintaining the original mechanical properties of the substrate.
Disadvantages: The zinc layer has weak adhesion (cross-cut test ≥4B level), and the corrosion resistance is only 1/3-1/2 of hot-dip galvanizing.
4. Performance requirements for typical application scenarios
ASTM A53: The yield strength of galvanized steel pipes is ≥250MPa (Grade B) and the minimum elongation is 18%.
EN 10217-1: The thickness of the hot-dip galvanized layer is required to be ≥85μm, and the impact test temperature is -20℃.
2. Chinese standards
GB/T 3091-2015: The uniformity test of the galvanized layer is ≥5 times of copper sulfate immersion without red rust.
GB/T 13793-2016: The flattening test of the straight seam electric welded steel pipe is pressed to 1/3 of the outer diameter without cracks.
6. Performance optimization direction
1. Alloying treatment
Adding 0.1-0.3% Al can refine the grains of the galvanized layer and improve the toughness by 10-15%.
The use of Zn-Al-Mg coating (such as Zn-55% Al-1.6% Si) can improve corrosion resistance by 3-5 times without reducing mechanical properties.
2. Surface treatment
Phosphating pretreatment can enhance the adhesion of the zinc layer, and the cross-cut test can reach 5B level.
Coating epoxy resin (300-500μm) can simultaneously improve corrosion resistance and wear resistance.
VII. Summary and suggestions
1. Performance characteristics
The comprehensive mechanical properties of hot-dip galvanized pipes are slightly lower than those of the substrate, but the corrosion resistance is improved by 5-10 years.
Electro-galvanized pipes maintain the performance of the substrate, but require regular maintenance.
2. Selection suggestions
Select hot-dip galvanized Q345B for high corrosion environments, and select calm steel (such as Q235D) for low-temperature toughness requirements.
Precision mechanical parts should preferably select electro-galvanized seamless steel pipes.
3. Data limitations
The softening of the weld heat affected zone (HAZ) needs to be considered in actual engineering (hardness decreases by 15-20%).
The mechanical properties of girth welds of large diameter steel pipes (DN ≥ 300) need to be verified.
https://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.png00WLDSTEELhttps://www.wldsteel.com/wp-content/uploads/2020/10/wldsteel-logo.pngWLDSTEEL2025-04-01 07:32:222025-04-01 07:32:38Mechanical Properties Analysis Of Galvanized Steel Pipes


 Korean
 English
 Arabic
 Dutch
 French
 German
 Italian
 Spanish
 Japanese
 Portuguese
 Russian
 Thai
 Vietnamese